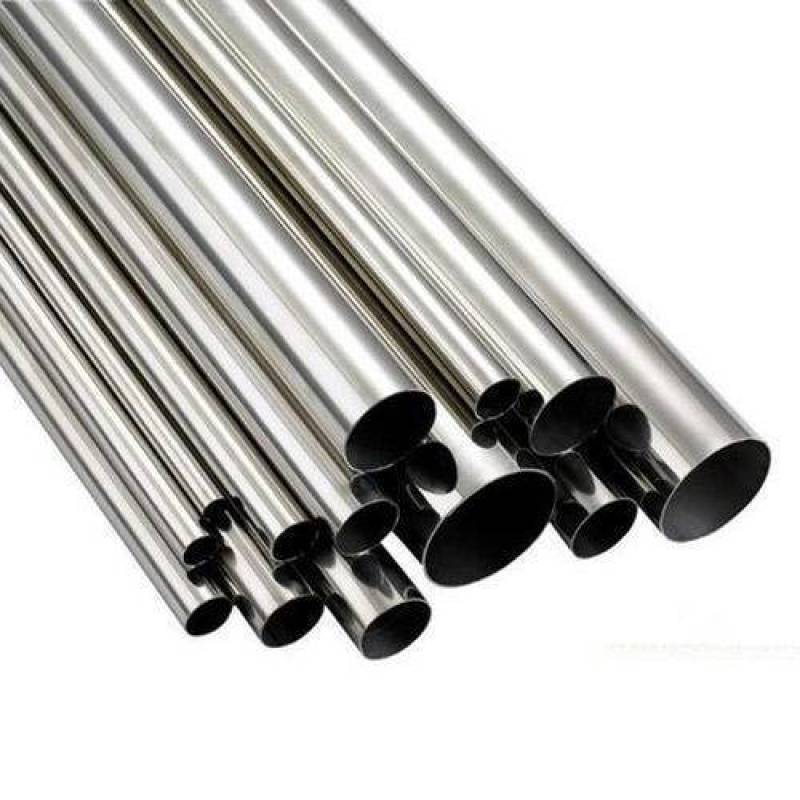
Siddhgiri Overseas manufactures Stainless Steel Seamless Tubes from our Mumbai facility, produced without any welded joint by piercing a solid billet into a hollow "mother tube" and then cold-drawing it through precision dies to final size. The absence of a weld seam means no heat-affected zone and uniform mechanical properties around the entire circumference, which is why seamless construction is specified wherever a joint would be a weak point — high-pressure lines, hydraulic and pneumatic systems, instrumentation tubing, and heat exchanger or condenser bundles. Manufactured to standards such as ASTM A213 and ASTM A269, our seamless tubes are supplied to precise outside diameter and wall thickness tolerances in SS 304, 304L, 316 and 316L grades, with the surface finishes and lengths required for critical industrial service. Established in 1962, Siddhgiri Overseas backs every batch with dimensional, hydrostatic and non-destructive testing before dispatch.
A stainless steel seamless tube is a hollow section produced with no longitudinal or spiral weld seam anywhere along its length. Instead of forming a strip and joining the edges, the tube is made by piercing a solid round billet to create a hollow shell, which is then reduced to final outside diameter (OD) and wall thickness through cold drawing or cold pilgering.
Because the tube wall is continuous solid metal formed from a single billet, there is no fusion zone, no heat-affected zone, and no filler material anywhere in the cross-section. Mechanical properties and corrosion resistance are consistent all the way around the circumference and along the full length of the tube — a characteristic that matters most in applications where a weld line would represent a point of relative weakness or a site for preferential corrosion.
Unlike stainless steel pipe, which is sized by nominal bore and schedule per standards such as ASTM A312, seamless tube is specified by its actual outside diameter and wall thickness. This is a defining difference between pipe and tube: pipe is chosen for flow capacity, tube is chosen for dimensional precision.
Seamless tube production begins with a solid stainless steel billet rather than a flat strip or coil. The billet is heated and pierced through its centre to produce a hollow shell — the "mother tube" — which already has an approximate OD and wall thickness but is far from the tolerances a finished tube requires.
Cold Drawing and Cold Pilgering
The mother tube is then reduced to its final dimensions through one or more cold-working passes:
Multiple drawing or pilgering passes are typically required to move from the mother tube's rough dimensions down to the fine OD and wall thickness called for on the drawing, with intermediate annealing between passes to relieve work hardening and restore ductility.
Heat Treatment, Pickling and Finishing
After final sizing, the tube undergoes controlled annealing to relieve internal stresses from cold working, refine grain structure and restore the material's designed corrosion resistance. Chemical cleaning and pickling then remove surface oxidation and scale, leaving a clean passivated surface. Precision straightening follows to ensure dimensional uniformity along the full length, and the tube is finished — bright annealed, pickled, satin or mirror polished — to the specification required.
Inspection
Every seamless tube is checked before dispatch, including dimensional inspection, hydrostatic pressure testing, eddy current or ultrasonic testing, chemical composition verification and visual examination, confirming the tube is free of defects and meets the applicable standard.
Both seamless and welded stainless steel tubes are manufactured by Siddhgiri Overseas, and the right choice depends on the demands of the application rather than one process being universally superior.
|
Starting stock |
Solid billet, pierced into a hollow mother tube |
Flat strip or coil, rolled and welded (TIG, laser or high-frequency) |
|
Weld seam |
None — continuous solid wall |
Longitudinal weld seam runs the full length |
|
Property uniformity |
Uniform strength and corrosion resistance around the full circumference |
Very good, but the weld zone is a distinct microstructural region |
|
Typical use case |
High-pressure lines, instrumentation, hydraulics, heat exchangers, applications where a seam is a purity or integrity risk |
Structural work, furniture, general fabrication, moderate-pressure service where cost efficiency matters |
|
Production cost |
Higher — billet piercing plus multiple cold-drawing or pilgering passes |
Lower — continuous strip forming and welding is a faster process |
Seamless tube costs more to produce because it requires billet piercing and additional cold-working passes to reach final dimensions, but it eliminates weld-related risk entirely — no weld metallurgy to qualify, no heat-affected zone, and no seam to act as a starting point for corrosion or fatigue cracking. Where process purity, pressure integrity or dimensional consistency around the full circumference outweighs the cost difference, seamless is the correct specification.
Because seamless tube has no weld seam to act as a weak point, it is specified in service conditions where pressure integrity, purity or dimensional precision are non-negotiable.
Siddhgiri Overseas supplies seamless stainless steel tube in SS 304, 304L, 316 and 316L to the OD, wall thickness and finish required for these applications, tested and inspected before dispatch.
Siddhgiri Overseas is ISO certified for quality, occupational health & safety and environment management, and holds the import and export certification required to supply stainless steel pipe and tube to customers worldwide. Certificate copies are available on request for buyers who need them for their own compliance records.
A seamless tube is formed from a solid billet that is pierced into a hollow mother tube and then cold-drawn or cold-pilgered to final size, so there is no longitudinal weld seam anywhere in the tube wall. A welded tube, by contrast, is made by rolling flat strip into a cylinder and joining the edges with a weld.
Because the tube wall is continuous solid metal with no weld seam, there is no heat-affected zone and no fusion boundary to act as a weak point under pressure. Strength and corrosion resistance are uniform around the full circumference, which is why seamless tube is specified for hydraulic systems, high-pressure process lines and instrumentation.
Our seamless stainless steel tubes are produced to standards including ASTM A213 for ferritic and austenitic alloy steel boiler and heat-exchanger tubes, and ASTM A269 for seamless and welded austenitic tubing used in general service, along with other applicable ASTM, ASME, DIN, EN and JIS specifications as required by the project.
Seamless tube is specified by its actual outside diameter (OD) and wall thickness. This differs from stainless steel pipe, which is sized by nominal bore and schedule under standards such as ASTM A312. Tube sizing gives the tighter dimensional control needed for precision engineering, instrumentation and heat-exchanger applications.
Siddhgiri Overseas manufactures seamless tube in SS 304 and 304L for general corrosion resistance and fabrication work, and SS 316 and 316L, which contain molybdenum for enhanced resistance to chlorides, acids and marine or process-chemical environments.
Yes — seamless tube requires billet piercing and additional cold-drawing or cold-pilgering passes, which makes it more expensive to produce than welded tube. The trade-off is justified whenever a weld seam would pose a pressure-integrity, purity or reliability risk, such as in instrumentation lines, hydraulic systems and heat exchanger tubing.
Every batch undergoes dimensional inspection, hydrostatic pressure testing, eddy current or ultrasonic testing, chemical composition analysis, mechanical strength testing and visual examination, ensuring each tube meets the specified standard before it leaves our Mumbai facility.
We supply seamless tube in bright annealed, pickled, matte, satin and mirror-polished finishes, selected according to the application — process and hygienic applications typically favour bright annealed or pickled finishes, while architectural or decorative uses may call for a mirror polish.