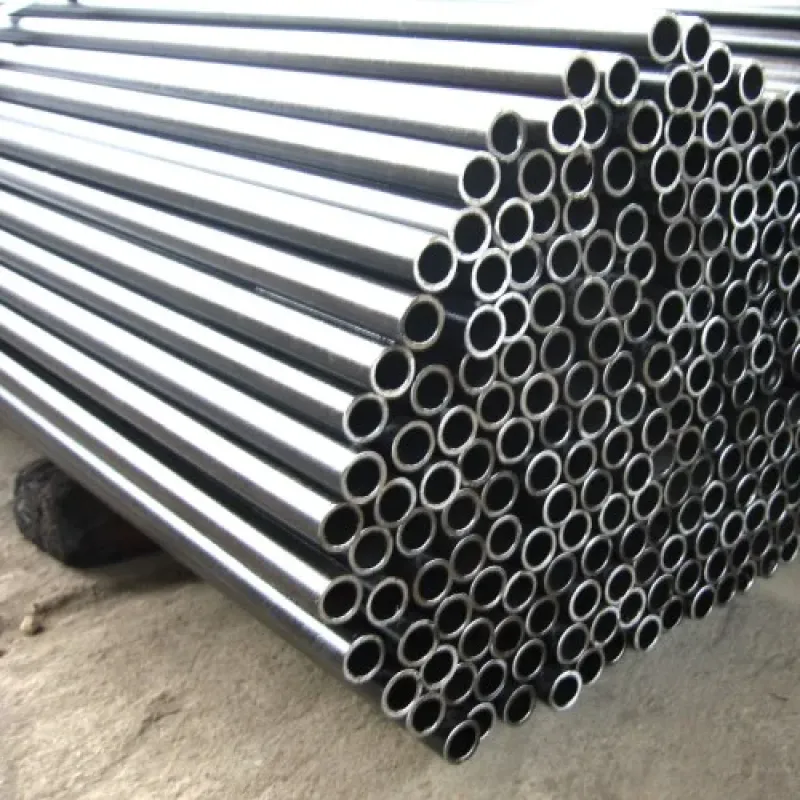
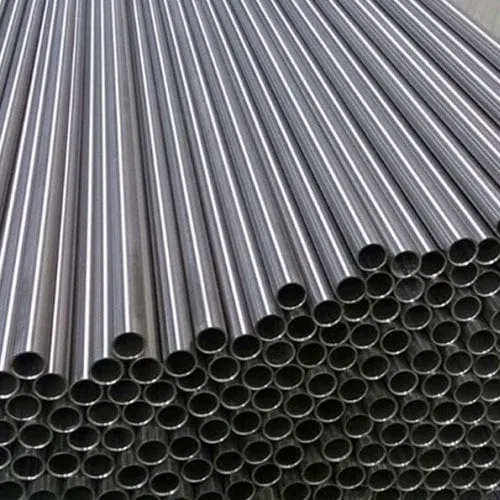
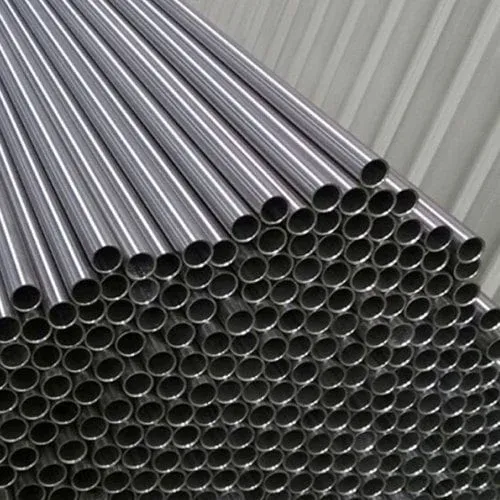
Siddhgiri Overseas manufactures SS 310 Tube from our Mumbai facility for applications where sustained, extreme heat — not corrosion resistance alone — is the governing condition. Built on an austenitic chemistry of 24-26% chromium and 19-22% nickel, SS 310 tube holds a stable, adherent oxide layer in dry air at continuous service temperatures up to around 1150°C, well beyond the point where standard grades such as SS 304 and SS 316 begin to scale and lose structural integrity. Our seamless and welded tubes are cold-drawn and roll-formed on our own production lines to ASTM A213, ASTM A249 and equivalent ASME specifications, in standard SS 310 and low-carbon SS 310S chemistries, for furnace, kiln, boiler and heavy thermal-processing service. Established in 1962, every batch is tested and dispatched with full material documentation from our Mumbai works.
SS 310 tube is a high-chromium, high-nickel austenitic stainless steel tube engineered for continuous service at temperatures well beyond the range that general-purpose grades can tolerate. Where most stainless tube is selected for corrosion resistance or mechanical strength at ambient-to-moderate temperatures, SS 310 exists to solve a different problem: staying structurally sound and dimensionally stable while sitting in furnace-level heat for extended periods, cycle after cycle.
That capability comes directly from its alloy content. Chromium at 24.0-26.0% and nickel at 19.0-22.0% — both substantially higher than in standard austenitic grades — form a dense, tightly adherent oxide scale that continues to protect the base metal as temperature rises rather than breaking down and flaking off. In dry air, this allows SS 310 tube to run continuously at approximately 1150°C, with intermittent service up to around 1035°C, placing it among the standard refractory-grade stainless steels used across furnace, kiln and heavy thermal-processing industries.
Siddhgiri Overseas manufactures SS 310 tube in seamless form — cold-drawn from solid billet on our own cold-drawing plants with no weld seam — as well as welded (ERW and EFW) construction from our high-frequency roll-forming and fusion-welding lines, so the tube type can be matched to the pressure and fabrication requirements of the project. The low-carbon SS 310S variant (0.08% carbon maximum) is produced specifically for tubes that undergo extensive field welding, since low carbon content restricts carbide precipitation at the weld zone and reduces the risk of embrittlement over the tube's service life. SS 310 also retains useful toughness and low magnetic permeability at cryogenic temperatures down to -267°C, giving the grade a genuinely wide operating range at both extremes.
SS 310 tube from Siddhgiri Overseas is produced to the following chemical composition, with the standard and low-carbon SS 310S limits shown separately:
|
Chromium (Cr) |
24.00% - 26.00% |
Primary defense against oxidation and scaling, effective up to roughly 1150°C |
|
Nickel (Ni) |
19.00% - 22.00% |
Stabilises the austenitic structure and resists scale flaking through repeated thermal cycling |
|
Manganese (Mn) |
2.00% max |
Standard alloying control element |
|
Carbon (C) |
0.25% max (standard) / 0.08% max (310S) |
Governs weldability and risk of carbide precipitation at the weld zone |
Mechanical properties: minimum tensile strength of 515 MPa (75 ksi) and minimum yield strength of 205 MPa (30 ksi), with hardness limited to Rockwell B (HRB) 95 maximum or Brinell (HBW) 217 maximum.
Standards: our SS 310 / 310S tubes are manufactured to ASTM A213 (seamless ferritic and austenitic alloy-steel tubes for boilers, superheaters and heat exchangers), ASTM A249 (welded austenitic tubes for boiler, superheater, heat exchanger and condenser service) and the corresponding ASME SA213 and SA249 specifications, with dimensions governed by ANSI B36.19M and related standards.
Available range: outside diameters from small-bore capillary and instrumentation sizes up to large structural sizes, wall thickness from approximately 0.3 mm to 50.0 mm, in schedules including 5S, 10S, 40S, 80S and 160, supplied with end configurations (plain, bevelled or threaded) and surface finishes (No.1 pickled, 2B matte, bright annealed or mechanically polished) to suit the application.
Testing: production lots are verified through hydrostatic testing, eddy current or ultrasonic examination, and Positive Material Identification (PMI) to confirm chromium-nickel chemistry, with radiography available where full weld-seam integrity must be documented. Every order is accompanied by a Mill Test Certificate.
Siddhgiri Overseas manufactures SS 310 tube across several construction methods, chosen according to the fluid dynamics, operating pressure and fabrication requirements of the application.
Seamless (SMLS): extruded from solid steel billet with no longitudinal weld line, then cold-drawn on our own cold-drawing benches to tight dimensional tolerances. Preferred for high-pressure boilers, radiant tubes and heat exchangers, where the absence of a weld eliminates any heat-affected weak point.
Electric Resistance Welded (ERW): continuous stainless strip formed into shape and welded along the seam using high-frequency electricity on our automatic roll-forming lines. A cost-effective option for flue gas ducting and large-array installations requiring narrow dimensional tolerances.
Electric Fusion Welded (EFW): produced from heavy steel plate using high-energy electric arc welding and fully radiographed to confirm complete weld penetration, suited to larger industrial kiln and furnace assemblies.
Cold Drawn Welded (CDW): the welded base tube is drawn through a precision die over an internal mandrel, refining grain alignment at the weld seam so that mechanical properties are consistent along the full length of the tube.
SS 310 tube is specified wherever a component must retain its strength and resist oxidation under continuous or cyclic extreme heat — conditions in which standard austenitic grades such as SS 304 and SS 316 suffer visible scaling and structural degradation.
Siddhgiri Overseas supplies SS 310 tube in round, square and rectangular sections, and in seamless, ERW and EFW construction, matched to the operating pressure, temperature profile and fabrication method of the customer's system.
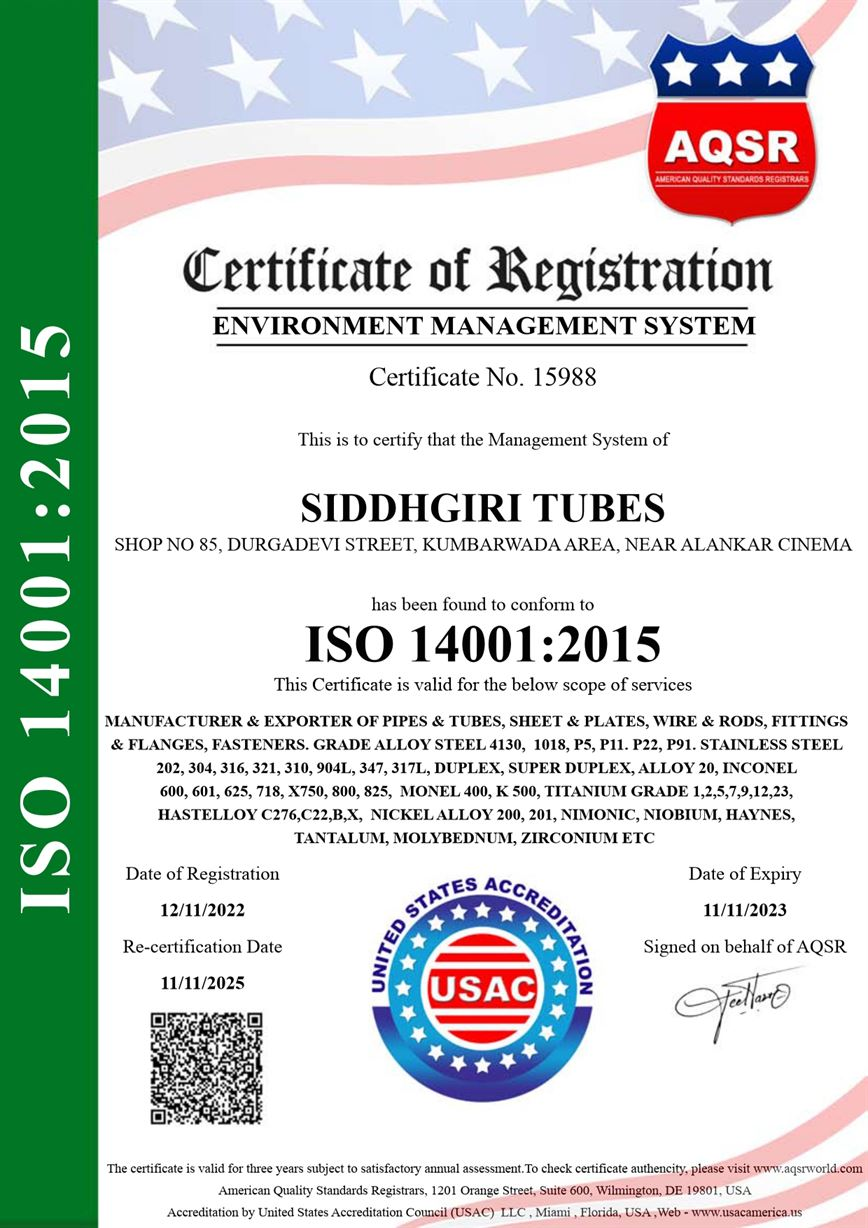
Siddhgiri Overseas is ISO certified for quality, occupational health & safety and environment management, and holds the import and export certification required to supply stainless steel pipe and tube to customers worldwide. Certificate copies are available on request for buyers who need them for their own compliance records.
SS 310 tube resists oxidation and retains mechanical strength in dry air at continuous service temperatures up to approximately 1150°C, with intermittent exposure tolerated up to around 1035°C, making it one of the standard refractory-grade stainless tubes for sustained high-heat service.
The difference is carbon content. Standard SS 310 carries up to 0.25% carbon, while SS 310S is a low-carbon variant capped at 0.08% carbon. SS 310S is specified when a tube will undergo extensive field welding, since the lower carbon content restricts carbide precipitation in the weld heat-affected zone and reduces the risk of embrittlement in long-term service.
SS 310's chromium content of 24-26% and nickel content of 19-22% are substantially higher than in SS 304 or SS 316, producing a denser, more stable oxide layer. This lets SS 310 continue performing reliably at temperatures where SS 304 and SS 316 begin to oxidise, scale and lose structural integrity, making SS 310 the correct choice for furnace, kiln and continuous high-heat applications.
Yes. Siddhgiri Overseas manufactures SS 310 tube as seamless (SMLS) tube cold-drawn from solid billet, as well as Electric Resistance Welded (ERW), Electric Fusion Welded (EFW) and Cold Drawn Welded (CDW) construction, so the tube type can be matched to the pressure rating and fabrication method required by the project.
Yes, using GTAW/TIG, GMAW/MIG or SMAW welding methods. For heavy field welding, the low-carbon SS 310S variant is generally recommended, as it does not require solution annealing after welding and carries a lower risk of carbide precipitation at the joint compared with standard SS 310.
Our SS 310 and SS 310S tubes are produced to ASTM A213 for seamless tubes and ASTM A249 for welded tubes, along with the corresponding ASME SA213 and SA249 specifications, with dimensions governed by ANSI B36.19M and related standards.
SS 310 tube is available from small-bore capillary and instrumentation sizes through to large structural diameters, with wall thickness ranging from approximately 0.3 mm to 50.0 mm across schedules including 5S, 10S, 40S, 80S and 160, in round, square and rectangular sections.
Every batch is verified through hydrostatic testing, eddy current or ultrasonic examination, Positive Material Identification (PMI) to confirm chromium-nickel chemistry, and radiography where weld-seam integrity must be documented, with a Mill Test Certificate issued from our Mumbai facility for each order.