Siddhgiri Overseas manufactures stainless steel seamless tube in Mumbai and supplies buyers in Cape Town. In continuous production since 1962.
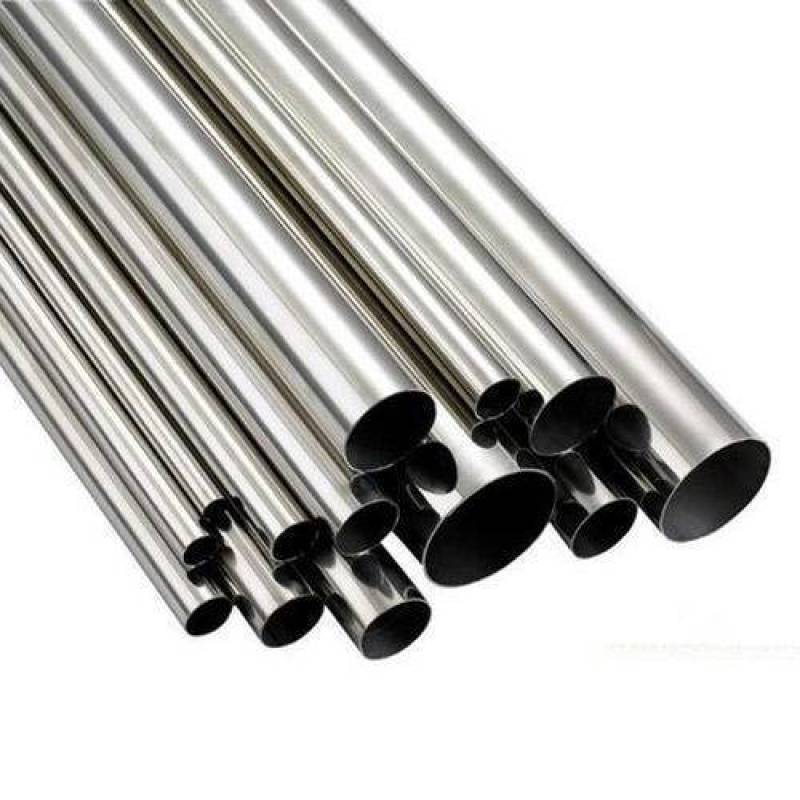
Seamless tube is made from a solid billet, pierced and worked down to size, so there is no longitudinal joint anywhere in the wall. For heat exchangers, hydraulic lines and high-pressure instrument work that absence is the whole reason the product exists.
Send the outside diameter, wall thickness, length, grade, quantity and the standard your drawing cites. Tube is ordered by actual dimensions rather than by nominal size, and getting that right at enquiry stage saves a return shipment.
The route matters because it explains both the cost and the tolerances you can expect.
A solid round billet is heated and pierced over a mandrel, producing a thick hollow shell. That shell is then elongated and reduced, by pilger milling or by cold drawing through a die over a plug, in successive passes with intermediate annealing between them. Each pass tightens the dimensions and refines the grain structure.
Nothing in that sequence creates a joint. There is no seam to test, no heat affected zone to anneal out, and no weld bead to remove from the bore.
Piercing a billet does not produce a perfectly centred hole. Real seamless tube has some wall eccentricity: the wall is thicker on one side than the other, within the tolerance the standard permits.
That matters more than most buyers expect. On a pressure calculation the thin side governs, so a tube at the permitted eccentricity limit has less margin than its nominal wall suggests. On a heat exchanger it shifts the thermal profile around the circumference. And on anything being machined or expanded into a tubesheet, it is the difference between a sound joint and a leak found at hydrotest.
If your design depends on it, state a wall eccentricity limit tighter than the standard default at enquiry stage. It is achievable, it costs more, and it cannot be sorted out after the tube is made.
Heat exchangers and condensers. A213 is the governing specification for seamless boiler, superheater and heat exchanger tube. No seam means no preferential corrosion line down the length of a tube that will spend thirty years in a shell.
High-pressure hydraulic and instrument lines. Pressure rating follows OD and wall, and a seamless wall behaves predictably under cyclic pressure where a seam is a fatigue initiation site.
Sour and critical service. Where NACE MR0175 governs, or a client specification prohibits a longitudinal weld outright, which on refinery and offshore work is common.
Tube that will be cold-formed. U-bends, coils and tight radii work the wall hard. A seam in the bend radius is a liability.
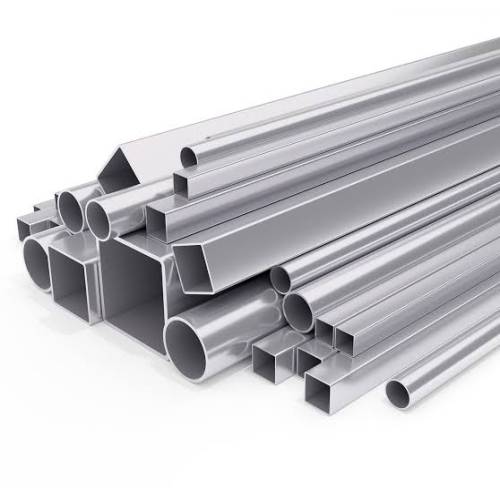
Worth saying plainly, because specifying seamless reflexively is expensive. For general corrosion-resisting service under A269, for structural and ornamental work under A554, for sanitary lines under A270, and for most low-pressure fluid handling, welded tube performs identically and costs materially less. It also holds a tighter wall tolerance, because strip is rolled to a closer thickness band than a pierced shell can be worked to.
Our stainless steel tube page covers the range across both constructions.
We supply seamless tube in 304, 304L, 316, 316L, 321, 310 and 347H, subject to size and availability.
A213 for boiler, superheater and heat exchanger tube. A269 for seamless and welded tube in general corrosion-resisting service. Where the drawing is written to a JIS or EN designation instead, send it as written rather than the ASTM grade you believe it maps to; the composition ranges overlap without being identical and the test regimes differ.
Pipe is specified by nominal pipe size and schedule. Tube is specified by actual outside diameter and wall thickness. Two inch tube measures 50.8 mm across the outside; NPS 2 pipe measures 60.3 mm. They are different products from different standards and they do not substitute for one another, however close the number on the drawing looks.
If the drawing gives a schedule, it means pipe. If it gives an OD and a wall, it means tube. Where a single project sheet mixes both, which happens whenever two consultants have worked on it, resolve it before the order rather than at goods inward.
Seamless tube production begins with a solid stainless steel billet rather than a flat strip or coil. The billet is heated and pierced through its centre to produce a hollow shell — the "mother tube" — which already has an approximate OD and wall thickness but is far from the tolerances a finished tube requires.
Cold Drawing and Cold Pilgering
The mother tube is then reduced to its final dimensions through one or more cold-working passes:
Multiple drawing or pilgering passes are typically required to move from the mother tube's rough dimensions down to the fine OD and wall thickness called for on the drawing, with intermediate annealing between passes to relieve work hardening and restore ductility.
Heat Treatment, Pickling and Finishing
After final sizing, the tube undergoes controlled annealing to relieve internal stresses from cold working, refine grain structure and restore the material's designed corrosion resistance. Chemical cleaning and pickling then remove surface oxidation and scale, leaving a clean passivated surface. Precision straightening follows to ensure dimensional uniformity along the full length, and the tube is finished — bright annealed, pickled, satin or mirror polished — to the specification required.
Inspection
Every seamless tube is checked before dispatch, including dimensional inspection, hydrostatic pressure testing, eddy current or ultrasonic testing, chemical composition verification and visual examination, confirming the tube is free of defects and meets the applicable standard.
Both seamless and welded stainless steel tubes are manufactured by Siddhgiri Overseas, and the right choice depends on the demands of the application rather than one process being universally superior.
|
Starting stock |
Solid billet, pierced into a hollow mother tube |
Flat strip or coil, rolled and welded (TIG, laser or high-frequency) |
|
Weld seam |
None — continuous solid wall |
Longitudinal weld seam runs the full length |
|
Property uniformity |
Uniform strength and corrosion resistance around the full circumference |
Very good, but the weld zone is a distinct microstructural region |
|
Typical use case |
High-pressure lines, instrumentation, hydraulics, heat exchangers, applications where a seam is a purity or integrity risk |
Structural work, furniture, general fabrication, moderate-pressure service where cost efficiency matters |
|
Production cost |
Higher — billet piercing plus multiple cold-drawing or pilgering passes |
Lower — continuous strip forming and welding is a faster process |
Seamless tube costs more to produce because it requires billet piercing and additional cold-working passes to reach final dimensions, but it eliminates weld-related risk entirely — no weld metallurgy to qualify, no heat-affected zone, and no seam to act as a starting point for corrosion or fatigue cracking. Where process purity, pressure integrity or dimensional consistency around the full circumference outweighs the cost difference, seamless is the correct specification.
Because seamless tube has no weld seam to act as a weak point, it is specified in service conditions where pressure integrity, purity or dimensional precision are non-negotiable.
Siddhgiri Overseas supplies seamless stainless steel tube in SS 304, 304L, 316 and 316L to the OD, wall thickness and finish required for these applications, tested and inspected before dispatch.
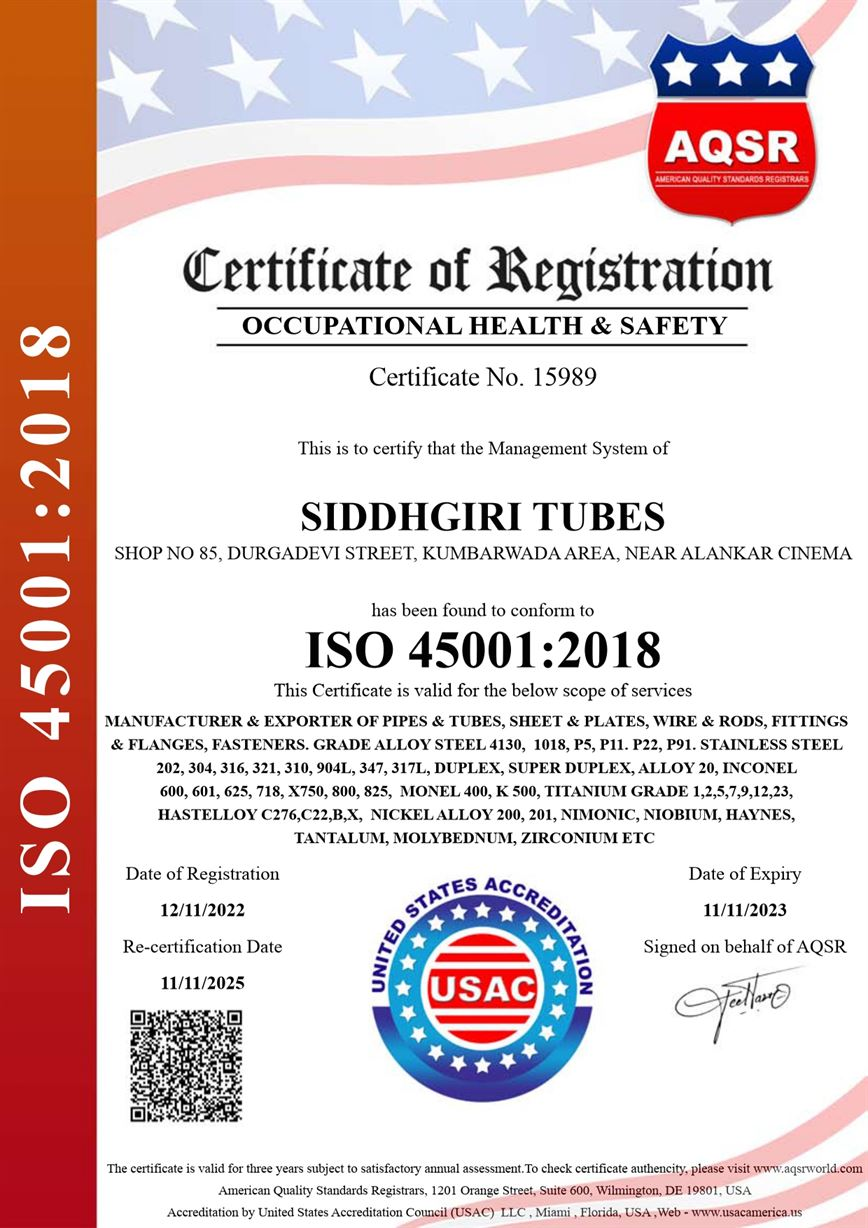
Siddhgiri Overseas is ISO certified for quality, occupational health & safety and environment management, and holds the import and export certification required to supply stainless steel pipe and tube to customers worldwide. Certificate copies are available on request for buyers who need them for their own compliance records.
Mill test certificates issued by the works, recording heat number, chemical analysis and mechanical test results for the batch, with the heat number matching the marking on the tube. The certificate guide sets out the EN 10204 types where your specification names one.
Siddhgiri Overseas is certified to ISO 9001, ISO 45001 and ISO 14001, with PED requirements applied to export material for pressure duty.
No. It is better for high pressure, cyclic duty, sour service and tight cold-forming. For general service, structural work and sanitary lines, welded tube performs the same, costs less and holds a tighter wall tolerance.
Whatever the standard permits, unless you specify tighter. If your pressure calculation or your tubesheet joint depends on a more uniform wall, say so at enquiry stage; it is a manufacturing decision, not an inspection one.
Yes, and for exchanger bundles that is normally how it is ordered. Send the cut length and the tolerance.
Send the bend radius, leg lengths and whether stress relief of the bend region is required. Bending cold-works the extrados and leaves residual tensile stress where chlorides concentrate, so on chloride duty above about 60 °C that stress relief is worth specifying.
Outside diameter, wall thickness, length and tolerance, grade, quantity, standard, surface condition, and any eccentricity or straightness requirement. For exchanger work, the tubesheet hole size and the joint type.
A seamless tube is formed from a solid billet that is pierced into a hollow mother tube and then cold-drawn or cold-pilgered to final size, so there is no longitudinal weld seam anywhere in the tube wall. A welded tube, by contrast, is made by rolling flat strip into a cylinder and joining the edges with a weld.
Because the tube wall is continuous solid metal with no weld seam, there is no heat-affected zone and no fusion boundary to act as a weak point under pressure. Strength and corrosion resistance are uniform around the full circumference, which is why seamless tube is specified for hydraulic systems, high-pressure process lines and instrumentation.
Our seamless stainless steel tubes are produced to standards including ASTM A213 for ferritic and austenitic alloy steel boiler and heat-exchanger tubes, and ASTM A269 for seamless and welded austenitic tubing used in general service, along with other applicable ASTM, ASME, DIN, EN and JIS specifications as required by the project.
Seamless tube is specified by its actual outside diameter (OD) and wall thickness. This differs from stainless steel pipe, which is sized by nominal bore and schedule under standards such as ASTM A312. Tube sizing gives the tighter dimensional control needed for precision engineering, instrumentation and heat-exchanger applications.
Siddhgiri Overseas manufactures seamless tube in SS 304 and 304L for general corrosion resistance and fabrication work, and SS 316 and 316L, which contain molybdenum for enhanced resistance to chlorides, acids and marine or process-chemical environments.
Yes — seamless tube requires billet piercing and additional cold-drawing or cold-pilgering passes, which makes it more expensive to produce than welded tube. The trade-off is justified whenever a weld seam would pose a pressure-integrity, purity or reliability risk, such as in instrumentation lines, hydraulic systems and heat exchanger tubing.
Every batch undergoes dimensional inspection, hydrostatic pressure testing, eddy current or ultrasonic testing, chemical composition analysis, mechanical strength testing and visual examination, ensuring each tube meets the specified standard before it leaves our Mumbai facility.
We supply seamless tube in bright annealed, pickled, matte, satin and mirror-polished finishes, selected according to the application — process and hygienic applications typically favour bright annealed or pickled finishes, while architectural or decorative uses may call for a mirror polish.