Phone Number +91-96194-06392
Opening Hours:

Mon-Sat: 9am - 6pm

SS 316L Tube Manufacturer in Uae United Arab Emirates

Import Export
European Directive 2014/68/EU
ISO 14001:2015
ISO 45001:2018
ISO 9001:2015
GST Certificate
SS 316L Tube Manufacturer in Uae United Arab Emirates

SS 316L Tube Manufacturer in Uae United Arab Emirates

Chemical Composition & Mechanical Properties

SS 316L tube is manufactured to a tightly controlled chemistry. A close control of chromium, nickel and molybdenum, together with a lowered carbon ceiling, is what removes the weaknesses of higher-carbon 316-series steel in welded service:

Chromium (Cr)

16.0% – 18.0%

Nickel (Ni)

10.0% – 14.0%

Molybdenum (Mo)

2.0% – 3.0%

Carbon (C)

0.03% max

Cross-referenced against other major standards, SS 316L corresponds to DIN/Werkstoff 1.4404, EN designation X2CrNiMo17-13-2, and ASTM/ASME grade TP316L. The "2" in the carbon designation is the key marker distinguishing it from standard 316 (1.4401 / X5CrNiMo17-12-2 / TP316), where the "5" reflects the higher permitted carbon level.

Mechanical and hardness thresholds for SS 316L tube are:

  • Tensile strength: 485 MPa minimum (70 ksi)
  • Yield strength: 170 MPa minimum (25 ksi)
  • Hardness: Rockwell B (HRB) 95 maximum, or Brinell (HBW) 217 maximum

Because carbon contributes to strength in austenitic stainless, these figures sit slightly below standard 316's higher-carbon strength levels — the trade-off for 316L's superior weld-zone stability. SS 316L also retains toughness and ductility at deep sub-zero and cryogenic temperatures, resisting the embrittlement that limits many other steel grades in cold service. Mill test certificates confirming chemical composition and mechanical properties are provided with each supply.
Manufacturing, Types & Standards

Producing SS 316L tube to specification depends on close control at every stage, from melt chemistry through final finishing:

  • Controlled molybdenum fusion: Vacuum oxygen decarburisation (VOD) and argon oxygen decarburisation (AOD) refining are used to distribute the 2.0%–3.0% molybdenum content uniformly through the steel matrix, which is what delivers consistent pitting resistance along the full tube length.
  • Solution annealing: Tubes are solution annealed between roughly 1040°C and 1150°C followed by rapid water quenching. This stabilises the austenitic grain structure and restores the corrosion resistance and ductility that cold working would otherwise reduce.
  • Cold drawing: Precision cold-draw benches and mandrel dies bring the tube to its final OD, wall thickness and surface finish, with intermediate annealing between passes where multiple reductions are required.

SS 316L tube is supplied in the following constructions:

  • Seamless tube: Drawn from a solid billet with no longitudinal weld line, giving uniform properties around the full circumference — specified for high-pressure hydraulic circuits, instrumentation and critical thermal duty to ASTM A213.
  • Welded tube: Roll-formed from flat strip and welded along the seam (ASTM A249 for boiler/heat-exchanger tube, ASTM A269 for general-service tube), offering close dimensional tolerances for larger-volume supply.
  • Cold-drawn welded (CDW) tube: A welded base tube drawn through a die and over an internal mandrel to refine the weld-seam microstructure, improving concentricity and surface finish.

Every batch is verified with hydrostatic testing, eddy current or ultrasonic testing, and Positive Material Identification (PMI) spectrometry to confirm the low-carbon chemistry before dispatch, with radiographic examination applied to welded tube as required.

Applications

SS 316L tube is specified wherever pitting resistance, weld-decay resistance and mechanical reliability are needed together in demanding service:

  • Marine and offshore infrastructure: Offshore platform piping, subsea hardware, desalination systems and coastal industrial plant exposed to continuous chloride and salt-spray attack.
  • Chemical and acidic process systems: Transport lines carrying organic acids, chloride-bearing compounds, industrial solvents and hot chemical mixtures, where welded joints must hold corrosion resistance under sustained exposure.
  • High-purity, pharmaceutical and food-grade manufacturing: Fluid lines in pharmaceutical processing, biotechnology, brewing and food production, where a smooth, low-carbon, non-contaminating bore is essential.
  • Instrumentation and heat exchanger tubing: Pressure and temperature sensing lines and heat-exchanger or condenser bundles, where dimensional precision and a defect-free bore support accurate, long-term performance.
  • Cryogenic and low-temperature service: SS 316L's low-carbon austenitic structure retains toughness at deep sub-zero temperatures, extending its use into cold-service systems within the same industries.

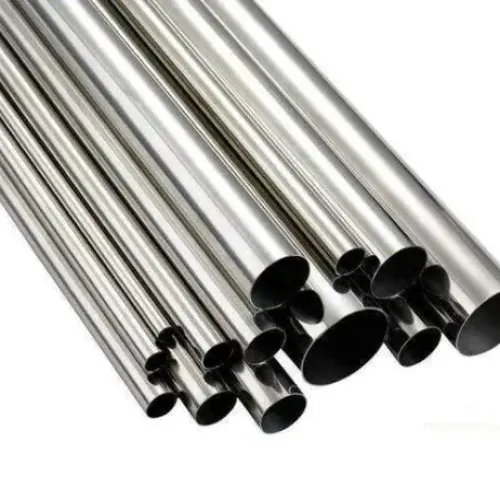
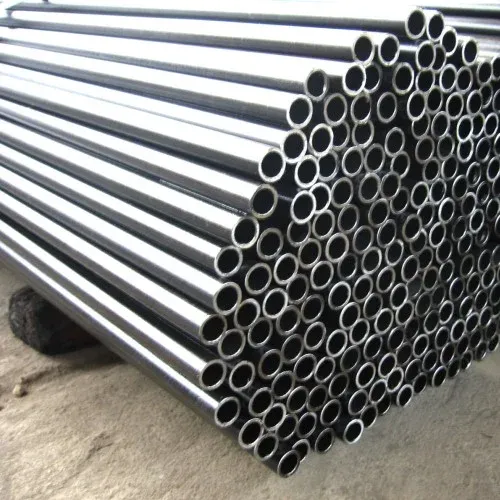
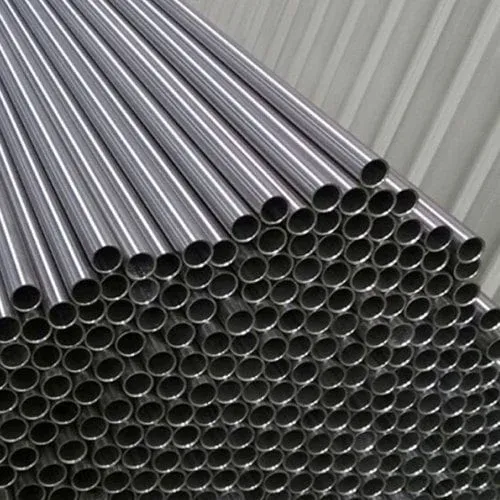
Siddhgiri Overseas supplies SS 316L tube in seamless and welded construction, in the OD, wall thickness and finish required for these applications, with testing and documentation completed before dispatch from our Mumbai facility.

Certifications

Siddhgiri Overseas is ISO certified for quality, occupational health & safety and environment management, and holds the import and export certification required to supply stainless steel pipe and tube to customers worldwide. Certificate copies are available on request for buyers who need them for their own compliance records.

Related Categories

FAQs

Frequently Asked Questions About SS 316L Tube

The compositional difference is carbon content: 0.03% maximum in 316L versus 0.08% maximum in standard 316. The molybdenum addition of 2.0%–3.0% that provides chloride and pitting resistance is identical in both grades. The lower carbon in 316L prevents chromium carbide precipitation at welded joints, so it holds its corrosion resistance through the heat-affected zone where standard 316 can be more vulnerable to weld decay.

When austenitic stainless is heated to roughly 425°C–870°C during welding, carbon can combine with chromium at the grain boundaries and precipitate as chromium carbides — a process called sensitization. This depletes the heat-affected zone of the chromium needed for corrosion resistance and can lead to intergranular attack, or weld decay, over time. SS 316L's low carbon content starves this reaction, so it is the preferred grade wherever a tube will be welded into a system.

SS 316L tube is specified by its actual outside diameter (OD) and wall thickness, produced to standards such as ASTM A213, A249 and A269. This differs from stainless steel pipe, which is sized by nominal bore and schedule under standards such as ASTM A312. Tube sizing gives the tighter dimensional control needed for instrumentation, heat exchangers and precision mechanical work.

Our SS 316L tube is produced to ASTM A213 for seamless ferritic and austenitic alloy-steel boiler and heat-exchanger tubes, ASTM A249 for welded austenitic tube in similar service, and ASTM A269 for general-service seamless and welded austenitic tubing, along with the corresponding ASME specifications and DIN/EN cross-references.

Yes. The 2.0%–3.0% molybdenum content in SS 316L gives it strong resistance to chloride-induced pitting and crevice corrosion, which is why it is widely used on offshore platforms, subsea installations, desalination systems and coastal industrial plant. Because these systems are almost always fabricated by welding, 316L's low-carbon chemistry ensures that resistance holds through the welded joints as well as the parent tube.

Yes, SS 316L is a standard choice for pharmaceutical, biotechnology, brewing and food-grade tubing. Its low-carbon chemistry keeps welded sanitary joints free of the carbide precipitation that could otherwise compromise corrosion resistance and product purity, while its smooth bore supports the repeated cleaning and sterilization these systems require.

Siddhgiri Overseas supplies SS 316L tube in No.1 pickled, 2B matte, bright annealed, mechanically polished, electropolished and No.8 mirror finishes. Process and hygienic applications typically specify bright annealed or electropolished surfaces, while structural or general-service tube commonly uses a 2B or pickled finish.

Every batch undergoes dimensional inspection, hydrostatic pressure testing, eddy current or ultrasonic testing, Positive Material Identification (PMI) to confirm the low-carbon chemistry, and visual examination, with radiographic testing applied to welded tube as required. Mill test certificates are issued confirming chemical composition and mechanical properties for each supply.

Clients

Our Partners

Tata Power
Shell Global Solutions
ONGC
NRL
NTPC
NIOC
HP
JSL
Godrej
Bhel
Inoxium Tubi
24/7 we are here
Your Partner in Industrial Growth, Let’s get started today!