Innovation in Production Infrastructure: Across Regional Manufacturing Centers
Our production mills use Vacuum Oxygen Decarburisation (VOD) and Argon Oxygen Decarburisation (AOD) refining matrices for controlled molybdenum fusion. This provides uniform distribution of elemental molybdenum (2.0% to 3.0%) within the steel matrix, resulting in greatly enhanced localised pitting resistance.
Rigorous Solution Annealing: The raw tube is subjected to carefully controlled heating and cooling cycles between 1040°C and 1150°C with a very fast cooling speed. This is an advanced stabilisation technique in which the internal austenitic grain orientation is fixed and the maximum structural strength of the alloy is achieved.
Heavy-duty cold-draw benches and special mandrel matrices allow us to obtain very tight geometric tolerances, uniform wall thicknesses and remarkably smooth inner surface topographies.
316L Stainless Steel Pipe Specification
Our products are designed to meet international standards to ensure seamless plant integration, universal interchangeability and structural safety. This low-carbon austenitic piping is defined by the following primary dimensional, chemical and testing properties as listed in the technical matrix below:
| Specification Parameter | Technical Standard Matrix / Operational Metric |
|---|
| Standard Classifications | ASTM A312, ASTM A213, ASTM A249, ASME SA312, ASME SA213, ASME SA249 |
| Dimensional Metrics | ANSI B36.19M, ANSI B36.10M, ASME B36.19 |
| Outside Diameter (OD) | 1/8" NB to 24" NB; capillary & instrumentation lines from 6.00 mm to 914.4 mm |
| Wall Thickness Range | 0.3 mm up to 50.0 mm (Schedules 5S, 10S, 40S, 80S, 160, XXS) |
| Length Profiles | Single Random (5–7 meters), Double Random (10–14 meters), or Cut-to-Length |
| End Configurations | Plain End (PE), Beveled End (BE), Threaded (Male/Female), Threaded Both Ends (TBE) |
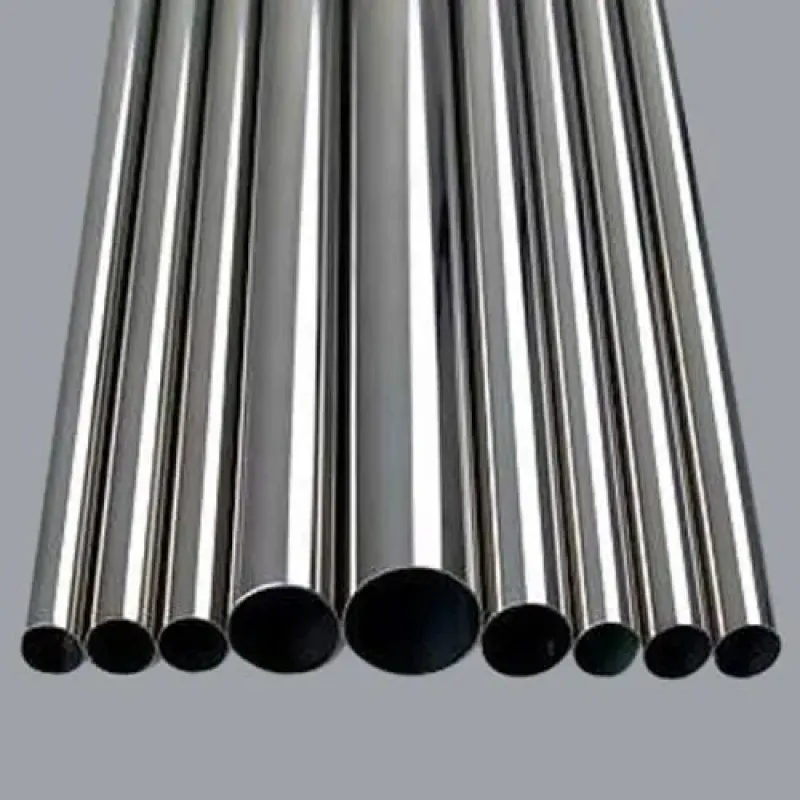
| Surface Finish States | No.1 Pickled (AP), 2B Matte, Bright Annealed (BA), Mechanically Polished (MP), Electropolished (EP), No. 8 Mirror Finish |
| Chemical Breakdown | Chromium (16.0%–18.0%), Nickel (10.0%–14.0%), Molybdenum (2.0%–3.0%), Carbon (0.03% Max) |
| Mechanical Thresholds | Tensile Strength: ≥ 485 MPa (70 ksi); Yield Strength: ≥ 170 MPa (25 ksi) |
| Hardness Limits | Rockwell B (HRB) ≤ 95 Max or Brinell Hardness (HBW) ≤ 217 Max |
| Testing Regimens | Hydrostatic, Eddy Current, Ultrasonic, Radiography (100% X-Ray), PMI Testing |
Metallurgy & Sensitization Immunity
It is the resistance of SS 316L to localised chemical attacks and to complete immunity to sensitisation that makes it unique. Standard 18-8 stainless steel types are acceptable for general use in atmospheric conditions but are extremely susceptible to fast localised corrosion when exposed to concentrated chloride or marine environments or aggressive industrial acids.
This is because 2.0–3.0% molybdenum is added, which intrinsically improves the surface chemistry of the alloy in a passive state. It acts in conjunction with chromium to form an extremely hard and self-healing chromium-molybdenum-oxide barrier. Moreover, the SS 316L has a very low limit of carbon (0.03%), which does not allow grain boundary precipitation during strong thermal cycles. This passive layer is effective in preventing the small chloride ions from producing localised pitting or crevice corrosion under severe operating conditions.
Available Product Configurations
Sidhgiri Overseas provides various structural designs of SS 316L pipe, depending on the requirements of fluid flow, pressure and economics:
Extruded without longitudinal weld lines, Seamless Pipes (SMLS): There are no heat-affected weak points in this seamless construction, which is the ideal solution for high-pressure hydraulic circuits, critical thermal loops, and sterile pharmaceutical networks.
Electric Resistance Welded (ERW): Roll-formed from flat steel sheets that are fused together by high-frequency electric resistance welding, this process is done in an automated manner. It offers a very economical solution for large-diameter utility and media lines, allowing for very close tolerances.
Heavy steel fabricating is done by using Electric Fusion Welding (EFW) : to create heavy steel plates with 100% radiograph monitoring to provide full penetration welds for heavy configurations.
Cold Drawn Welded (CDW): made by dragging a formed tube with a welded base through a precision die and mandrel. This improves the microstructural grain alignment at the seam to produce an excellent concentricity and surface finish smoothness.
316L Stainless Steel Pipe Price Index
International commodity exchanges have a significant impact on the commercial value of SS 316L piping products, especially in regard to the prices of key raw material commodities, such as elemental nickel and ferro-molybdenum futures, as well as specific fabrication options (e.g., high-speed automated roll-forming versus premium cold drawing).
Indicative Mill Pricing Structure (2026 Reference)
Premium Seamless Piping (ASTM A312 TP316L): It is available on a dimensional run scale and different specialised surface treatments with a price range of ₹380 to ₹480 per kilogram.
Welded/ERW Piping Lines (ASTM A312/A249): These are available at a cost of ₹330 to ₹430 per kg and are suitable for medium-pressure systems where budget is a concern.
Sample Procurement Reference Chart (Per-Meter Delivery Framework)
| Size Designation (NB) | Outside Diameter (OD) | Wall Thickness | Schedule Rating | Approximate Weight | Indicative Price (Tunisia) |
|---|
| 15 NB (1/2 Inch) | 21.34 mm | 2.11 mm | Schedule 10S | 1.02 kg/meter | ₹695 per Meter |
| 15 NB (1/2 Inch) | 21.34 mm | 2.77 mm | Schedule 40S | 1.29 kg/meter | ₹877 per Meter |
| 20 NB (3/4 Inch) | 26.70 mm | 2.11 mm | Schedule 10S | 1.33 kg/meter | ₹904 per Meter |
| 20 NB (3/4 Inch) | 26.70 mm | 2.87 mm | Schedule 40S | 1.75 kg/meter | ₹1,190 per Meter |
| 25 NB (1 Inch) | 33.40 mm | 2.77 mm | Schedule 10S | 2.13 kg/meter | ₹1,342 per Meter |
| 25 NB (1 Inch) | 33.40 mm | 3.38 mm | Schedule 40S | 2.54 kg/meter | ₹1,600 per Meter |
| 50 NB (2 Inch) | 60.33 mm | 2.77 mm | Schedule 10S | 3.99 kg/meter | ₹2,513 per Meter |
| 50 NB (2 Inch) | 60.33 mm | 3.91 mm | Schedule 40S | 5.52 kg/meter | ₹3,477 per Meter |
Tube Suppliers SS 316L in Tunisia
Sidhgiri Overseas, a leading SS 316L Tube Supplier in Tunisia and a certified stockholder, has a strong distribution network in the region. Our network reaches right down to the major industrial hubs and localised supply centres of {local_hubs}, which means on-site stockpiles of massive quantities that enable us to quickly allocate materials and eliminate long manufacturing lead times.
Precision Pre-processing: High-capacity band saws and precision arrays of laser cutters provide bevelled and pre-cut pipe for exact field dimensions.
Material Chemistry Validation: We use Positive Material Identification (PMI) spectrometers to confirm accurate alloy chemistry and ultra-low carbon levels before dispatch so that we can trace the steel back to the original steel melt.
Third-Party Inspector Collaboration: We coordinate product validation with top international inspection bodies like Bureau Veritas, TUV, SGS and Lloyd's Register on a regular basis to ensure it meets custom project requirements.
Industrial Packaging & Protective Protocols
Maintaining structural straightness, high-purity surface finishes, and accurate bevel geometry during long-haul handling and marine transportation are still major concerns.
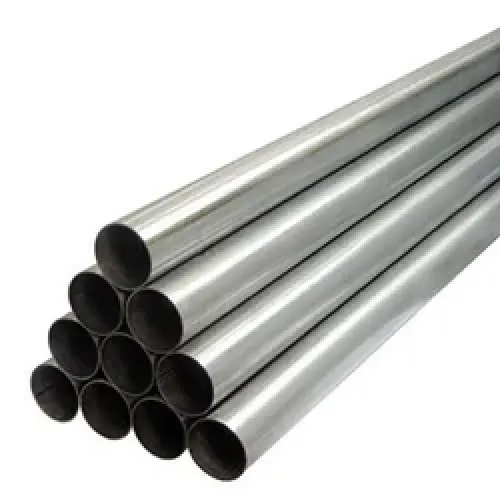
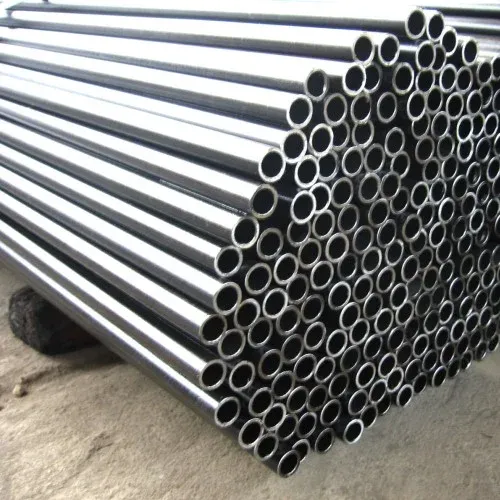
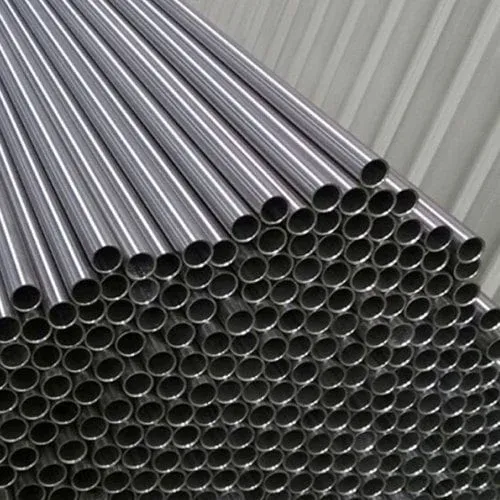
Secure Bundle Strapping: Hexagonal matrices of piping are tightly strapped and fitted with robust outer lifting slings, with high-density polyethylene (HDPE) plastic sheathing to prevent any metal-on-metal contact.
End Caps & Bevel Protection: Both ends of the exposed pipe are capped with heavy plastic caps which prevent debris from entering them and keep the vulnerable bevel angles of the pipe from being harmed by impact.
Heavy-Duty Crate Enclosures: Capillary tubes, instrumentation lines and electropolished or No. 8 mirror-polished tubes are packed in crates which are completely enclosed in wood with shock-absorbing internal packing.
Core Engineering Applications
Marine & Offshore Infrastructure: Used on offshore drilling rigs, subsea hardware assemblies, desalination plants and coastal industrial structures under severe marine salinity conditions.
Chemical & Acidic Engineering Systems: extensively applied for transport of aggressive organic acids, highly corrosive chloride compounds, industrial solvents and hot chemical mixtures.
High-Purity Manufacturing & Pharma: The only supplier for fluid lines for any pharmaceutical formulation, biotechnology laboratory, commercial brewing and food manufacturing application where product purity is critical.
Advanced Fabrication Processing
Cold Bending: Good ductility allows for smooth bending using rotary draw or mandrel machines. The material has a high work hardening rate and is processed by high-capacity stable hydraulic pressure.
Seamless Welding Integration: Readily weldable without the risk of intergranular corrosion using Gas Tungsten Arc Welding (GTAW/TIG), Gas Metal Arc Welding (GMAW/MIG) or conventional Shielded Metal Arc Welding (SMAW). The low-carbon chemistry results in corrosion resistance at the joint lines without any post-weld thermal treatment.
No. 2 – Pickling & Passivation: Immersing in the carefully controlled nitric/hydrofluoric acid bath after fabrication removes high-temperature scale and re-establishes the protective passive oxide surface layer.
Comprehensive Inventory Framework
For high-pressure fluid transport lines, processing loops and facility utility mains.
High-Purity Electropolished Tubing (EP): For pharmaceutical clean rooms, sterile biological environments and ultra-pure water loops.
Heavy-Wall Hydraulic Tubing: For chemical injection applications, high-pressure steam headers and heavy hydraulic manifolds.
SS 316L Tube Exporters in Tunisia
Sidhgiri Overseas is a leading SS 316L tube exporter in Tunisia and is operating under the complete compliance of the global standard frames. We routinely handle long-distance freight distribution of marine-grade piping solutions to industrial hubs throughout the Middle East, Southeast Asia, South America, Europe and North American distribution regions.
All export consignments are completed with detailed documentation, even mill test certificates for EN 10204 Type 3.1. Tight proximity to the primary seaports of the world provides quick customs clearance, safe stuffing of ocean containers and very predictable shipping times. Our extensive range of materials includes light and heavy wall profiles (Schedules 5S and 10S to 80S and 160s) that eliminate lead time for emergency plant turnarounds or fast-track construction schedules.
Detailed Dimensional Framework
316L Stainless Steel Pipe Pressure Rating
Maximum safe internal working pressures (psig) calculated via Barlow’s formula and governed by ASME B31.3 processing rules for seamless ASTM A312 TP316L pipes:
Comparison of the Properties of Ss 316 With Ss 316L.
As a specified case of the carbon threshold option, microstructural stability is important for assessing a large volume of welding in industrial assemblies:
Standard SS 316 (Carbon ≤ 0.08%): Slightly higher tensile strengths and better creep rupture properties after high-temperature exposures. It is, however, very susceptible to "sensitisation" in the range of 425°C to 860°C temperatures, where carbon can combine with chromium to form chromium carbides which, over time, cause weld decay.
SS 316L (Carbon ≤ 0.03%): The extra-low carbon variant. It gives better structural and chemical stability by complete elimination of carbide precipitation in the heat-affected zone (HAZ). This enables reliable multi-pass welding without the need for post-weld solution annealing.
316L tube and the welded-assembly case
316L is 316 with carbon held to 0.030% instead of 0.08%, the molybdenum
unchanged at 2–3%. On tube that distinction earns its keep more often
than it does on pipe, because tube assemblies are welded constantly: exchanger
tube-to-tubesheet joints, orbital-welded hygienic runs, instrument tubing
terminated in the field.
Every one of those welds is a chance to sensitise the heat affected zone,
and in 316 service the heat affected zone is precisely where chlorides will
concentrate. The low carbon removes the mechanism rather than managing it, with
no post-weld solution anneal required.
The cost is strength: A213 and A269 minima fall to 485 MPa
(70 ksi) tensile and 170 MPa (25 ksi) yield against 515 and 205
for 316, with 35% elongation. On a thin-wall tube under internal pressure that
can mean a heavier wall, so check it against the design code rather than
assuming the grades are interchangeable.
Dual-certified 316/316L tube, meeting both chemistries and both sets of
minima, is widely specified and is usually the practical answer where a
drawing is ambiguous.
316 against 316L, decided on the numbers
| Property | 316 | 316L | What it decides |
|---|
| Carbon, max | 0.08% | 0.030% | Whether the weld heat affected zone sensitises |
| Chromium | 16–18% | 16–18% | Unchanged |
| Nickel | 10–14% | 10–14% | Unchanged |
| Molybdenum | 2–3% | 2–3% | Unchanged; this is the chloride defence in both |
| Tensile, min | 515 MPa (75 ksi) | 485 MPa (70 ksi) | Wall thickness where allowable stress governs |
| Yield, min | 205 MPa (30 ksi) | 170 MPa (25 ksi) | As above |
| Elongation, min | 35% | 35% | Unchanged |
| Post-weld anneal | Often required | Not required | Fabrication cost and schedule |
Read down the last column and the decision makes itself. If the assembly is
welded and then sees chlorides, the carbon ceiling is the whole argument and
316L wins. If it is not welded, or is solution annealed after welding, 316
gives you 30 MPa more yield for the same money. Dual-certified 316/316L
material meets both chemistries and both sets of minima, and where a drawing
is ambiguous that is usually the practical answer.
Dairy, brewing and hygienic process tubing
Hygienic tube is a different product from process pipe that happens to be
316L, and ordering it as though it were the same is the commonest mistake on
these projects.
The standard is different. ASTM A270 covers sanitary
tube and carries requirements A269 and A213 do not. Dimensions commonly follow
the hygienic OD series rather than pipe sizes, so a "two inch" hygienic line
is 50.8 mm outside diameter.
Ra is the specification. Product-contact surfaces are
called out by internal roughness, typically in the 0.8 µm to
0.4 µm range depending on the duty, achieved mechanically or by
electropolishing. State the number and the method.
Orbital welding. Hygienic runs are welded autogenously
without filler, which means the tube's own chemistry and wall consistency
determine the weld. Tube supplied for orbital welding is held to tighter wall
tolerance for that reason, and ordering general-purpose tube for an orbital
installation causes weld problems that look like welder error.
End condition and protection. Ends capped, bore protected,
and the tube not used as a handrail on site before installation. Obvious, and
routinely ignored.
Passivation, electropolishing and the condition it arrives in
316L tube for clean service is bought in a surface condition, and the terms
are used loosely enough that orders go wrong.
Pickling removes scale and the chromium-depleted layer
under it with an acid treatment. It is a cleaning operation, and it leaves a
dull, matte surface.
Passivation is not cleaning. It is a controlled treatment,
usually nitric or citric acid, that removes free iron from the surface and lets
the chromium oxide film re-form evenly. Tube can be mechanically polished to a
fine Ra and still be contaminated with embedded iron from the polishing media,
which will bleed rust in service and look exactly like a material failure.
Specify passivation separately; a finish number does not imply it.
Electropolishing removes material electrochemically,
preferentially taking down peaks, which lowers Ra, rounds the surface profile
and leaves a chromium-enriched layer. It is the finish specified where
cleanability has to be demonstrable rather than asserted. It costs more and it
slightly increases the bore.
Order the three independently: mechanical finish as an Ra figure,
passivation as yes or no with the method, electropolishing as yes or no with
the target Ra. A line reading only "polished 316L tube" will be quoted against
the cheapest reading of it.
Why the bore matters more than the outside on 316L tube
On pipe the outside diameter is what everything connects to. On hygienic and
instrumentation tube the bore is the product: it is the surface the fluid
touches, the dimension the fitting seals against, and the thing that decides
whether a clean-in-place cycle actually cleans.
That inverts several ordering habits. Wall tolerance stops being a weight
question and becomes a bore-consistency question, because an orbital weld
between two tubes of slightly different wall will not fuse evenly. Internal
finish stops being cosmetic and becomes functional, because surface peaks
shelter residue that flow does not reach. And straightness stops being a
handling nicety and becomes an installation constraint on long runs.
When you send the enquiry, give the bore condition you need as explicitly as
the outside dimension: Ra target, whether passivated, whether electropolished,
and whether the ends are capped for transit. A quotation written against OD and
wall alone is pricing a different product.
Orbital welding, and what the tube has to do to support it
Hygienic 316L tube is joined autogenously: the torch fuses the two tube ends
together with no filler. That puts an unusual demand on the tube itself.
Wall consistency. With no filler to make up a difference,
two tubes with slightly different wall thickness at the joint will not fuse
evenly, and the weld will be thin on one side. Tube supplied for orbital work
is held to a tighter wall tolerance for exactly this reason, and ordering
general-purpose tube for an orbital installation produces weld failures that
look like operator error.
Sulphur content. This one surprises people. A trace of
sulphur in the melt changes the surface tension of the weld pool and therefore
how deeply it penetrates. Two heats both within the 316L specification can weld
quite differently, which is why controlled-sulphur tube is specified for
orbital work and why a bundle for one installation should come from the same
heat where possible.
Purge. The bore is the product surface. An unpurged root
leaves oxide on the inside of the joint, in the one place the process fluid
touches and nobody can reach to clean.
If the installation is orbital welded, say so at enquiry stage. It changes
which material is suitable, not just how it is joined.